Pingyilu Industrial Park, Nanguzhuangying Village, Ansu Town, Xushui District, Baoding City
Unlocking the Versatility of Stainless Steel Globe Valves in Various Applications
2025-04-19
The Unsung Heroes of Piping Systems
When it comes to managing the flow of liquids and gases, stainless steel globe valves are often the unsung heroes. These nifty devices not only regulate flow but also contribute to a system's overall efficiency. Whether you’re in the oil and gas sector, pharmaceuticals, or even food processing, globe valves play a critical role. Let's dive into the applications and benefits of these robust valves, shall we?
What Are Stainless Steel Globe Valves?
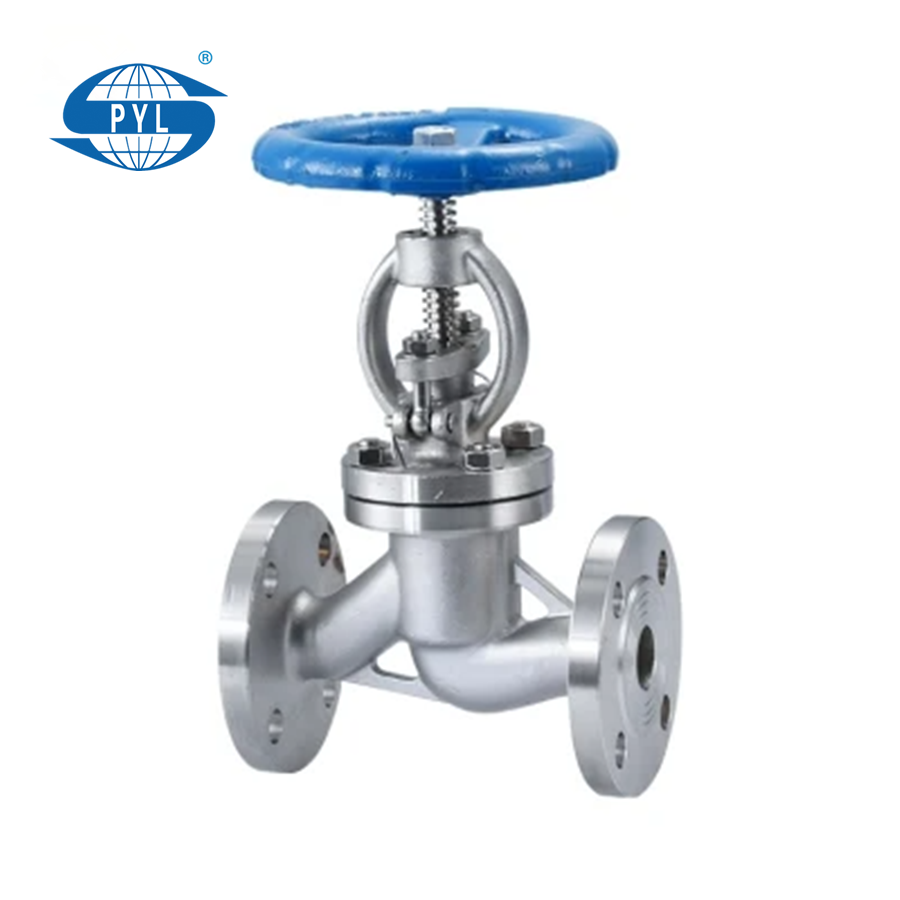
First things first, what exactly are stainless steel globe valves? Simply put, they’re a type of valve that utilizes a spherical body to control flow. The internal mechanism, comprising a movable disk and a stationary ring seat, allows for smooth and precise flow regulation. The use of stainless steel not only enhances durability but also provides excellent resistance to corrosion—ideal for harsh environments!
Where Are They Used?
Alright, let’s get into the nitty-gritty of applications. Here are some common scenarios where stainless steel globe valves are a must:
1. Oil and Gas Industry
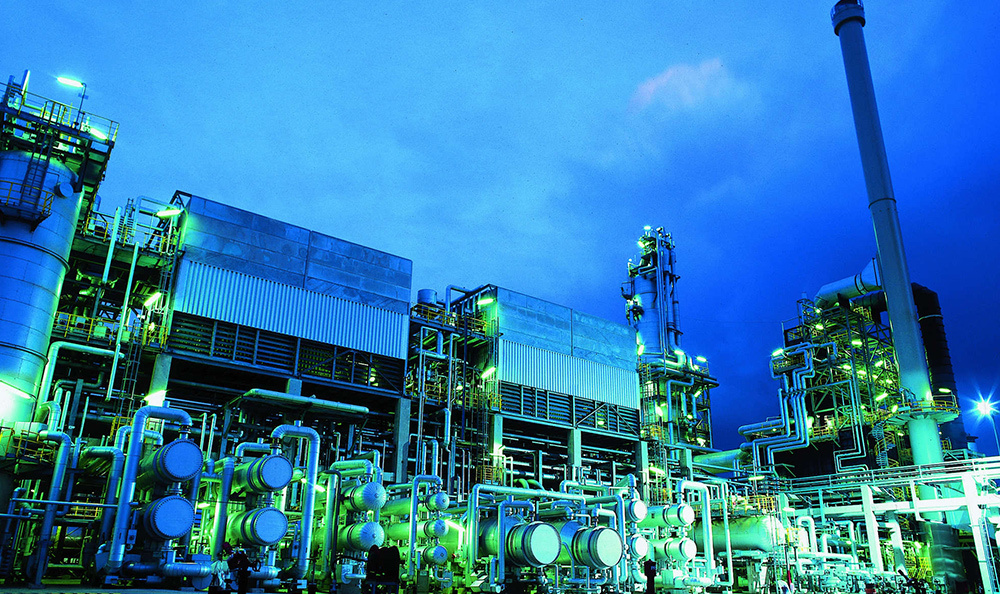
The oil and gas industry is a prime user of globe valves. With pipelines transporting crude oil or natural gas over vast distances, it’s crucial to have reliable flow control. These valves help ensure safety and functionality, providing operators with the ability to shut off flow quickly in emergencies. You could say they’re like the trusty sidekick in an action movie—always ready for action!
2. Water Treatment Plants
Water treatment plants also rely heavily on stainless steel globe valves to manage the flow of water during purification processes. They’re instrumental in controlling the flow rates and pressures, making sure that every drop is treated effectively. Talk about a vital role!
3. Food and Beverage Industry
In the food and beverage sector, cleanliness is next to godliness. Here, stainless steel valves are the preferred choice because they are easy to clean and sanitize, ensuring no contaminants enter the products. Plus, they can handle high temperatures and pressures, which is a significant advantage when processing hot liquids.
The Benefits of Choosing Stainless Steel Globe Valves
Now that we’ve covered where these valves are used, let’s talk benefits. Why should you consider investing in stainless steel globe valves? Here are a few reasons that might just tip the scale:
- Durability: Stainless steel is known for its strength and longevity, making these valves a sound investment.
- Corrosion Resistance: The material is naturally resistant to corrosion, which is a game-changer in many environments.
- Precise Flow Control: The design allows for fine adjustments, ensuring that flow rates are just right.
Installation and Maintenance Tips
Alright, let’s wrap this up with some practical advice. Installing stainless steel globe valves isn’t rocket science, but it does require attention to detail. Here’s what you need to keep in mind:
- Always ensure the valve is installed in the correct orientation. An upside-down valve? No thanks!
- Regularly check for leaks and wear. Prevention is better than cure, right?
- Keep the valve clean and free from debris. A little maintenance goes a long way!
Conclusion
In a nutshell, stainless steel globe valves are indispensable in a myriad of applications, from oil rigs to food processing plants. Their versatility, durability, and efficiency make them a top choice for many industries. So, the next time you turn on a tap or watch oil flow through a pipeline, remember the little valve that makes it all possible. Cheers to that!
Key words:
Hot News

More applications
Our corporation is the provincial-level enterprise,which owns the power to engage in import and export trade.


Contact Us
Telephone:+86-312-8587089
E-mail:pingyilu11@pylfm.com
Mobile/WeChat:+86-13933976795
Address: Pingyilu Industrial Park, Nanguzhuangying Village, Ansu Town, Xushui District, Baoding City

Add friends
Add friends